DCEN vs DCEP in TIG Welding Guide | TIG Welding Secrets
DCEN vs DCEP in TIG Welding: A Practical Polarity Guide
TIG Polarity Guide: DCEN vs DCEP Defined
Direct current polarity in TIG, or GTAW, describes where the tungsten sits in the electrical circuit. DCEN means Direct Current Electrode Negative, also called straight polarity: the torch is negative and the workpiece is positive. DCEP means Direct Current Electrode Positive, or reverse polarity: the torch is positive and the workpiece is negative. For a complete beginner setup guide, see the beginner TIG welding guide. With an electrode-negative setup, electrons flow from the tungsten to the work and put most of the heat into the joint, so you get deeper penetration. With DCEP, electrons flow from the work to the tungsten. That heats the electrode heavily and creates a strong cathodic cleaning effect on the surface, but penetration suffers. This guide explains what those two settings do and when to use each one.
Heat Distribution, Penetration, and Cleaning Action
Why Electrode-Negative Polarity Penetrates Deeper
With DCEN, roughly 70–80% of the heat is concentrated on the positive side of the arc—the workpiece—while only 20–30% reaches the tungsten. That creates a tighter, more focused arc and a deeper keyhole, which suits steel, stainless steel, titanium, nickel alloys, and most copper alloys. Because the tungsten stays cooler, you can use a smaller electrode at higher current without melting the tip. The result is a narrow, controllable puddle with strong penetration and little tungsten erosion. For most DC TIG work, this is the starting point in your polarity guide.

Why DCEP Cleans Aluminum
In DCEP, the workpiece is negative, or the cathode, and positive ions in the plasma strike the surface and disrupt the oxide film. This cathodic cleaning creates the familiar white, frosted etch zone on aluminum. The trade-off is serious, though: the tungsten becomes the anode and absorbs most of the heat. Penetration is shallow, the arc gets wider, and the tungsten can overheat or ball at modest amperage. So DCEP by itself is rarely used for structural joints. It is mainly reserved for specialized cleaning, very thin aluminum foil, or the EP portion of AC TIG. That distinction is one of the most important points in any TIG polarity guide.
- DCEN (electrode negative): deeper penetration, cooler tungsten, and minimal cleaning.
- DCEP (electrode positive): strong oxide cleaning, shallow penetration, and very hot tungsten.
- AC TIG alternates EN for penetration and EP for cleaning; balance control adjusts the mix.
Choosing and Preparing Tungsten for DCEN and DCEP
Tungsten type and tip geometry directly affect arc shape and electrode life. For electrode-negative work on steel and most nonferrous metals, except surfaces covered with aluminum oxide, 2% lanthanated (blue) or 2% ceriated (gray) electrodes work very well. They offer reliable starts and good stability at low to moderate current. 2% thoriated (red) tungsten is still common for DC work, but it is slightly radioactive, so follow appropriate handling precautions and local regulations. With DCEP, or the EP portion of AC aluminum work, the tungsten sees extreme heat. You need a larger diameter and a more durable tip shape. Use this tungsten guide as a starting point, then follow the limits listed by your machine and electrode manufacturer.
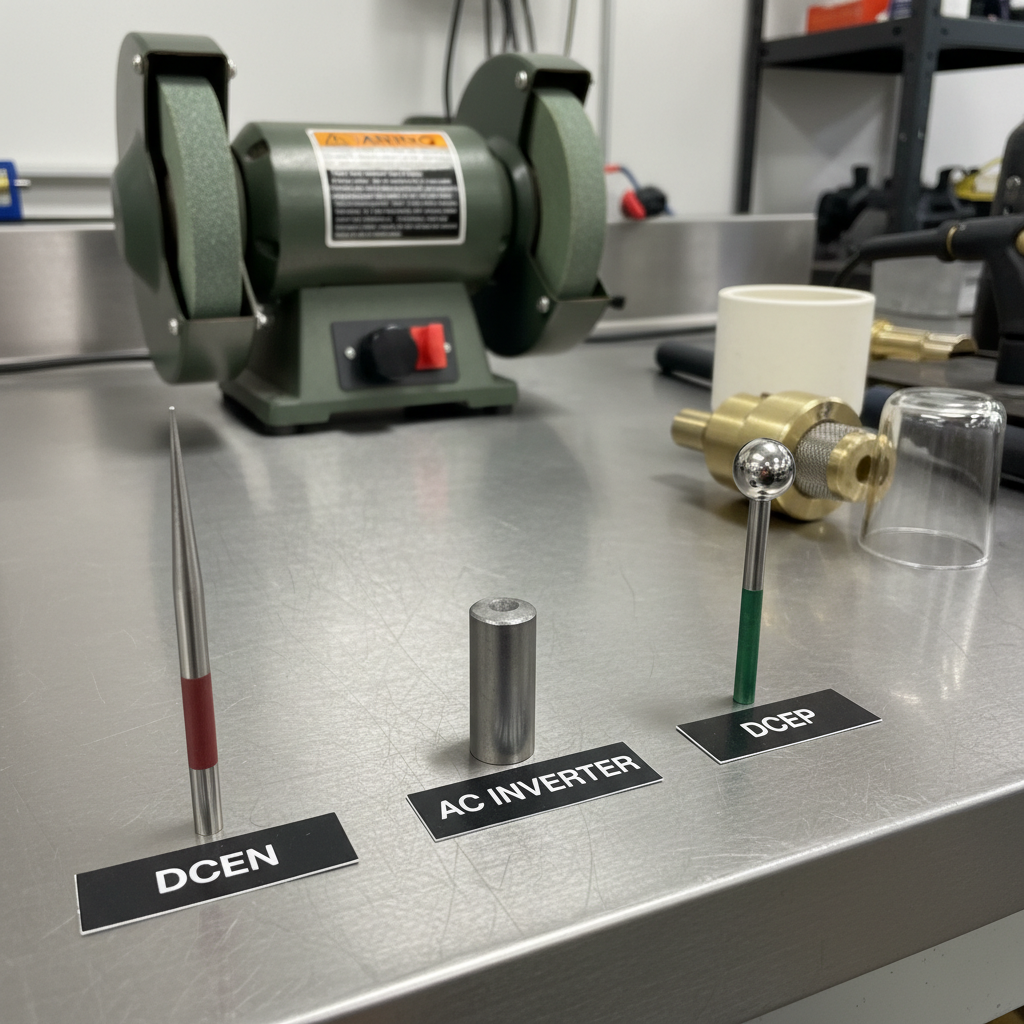
For DCEN, grind lengthwise to make a long taper about 2.5–3 times the electrode diameter, then add a tiny flat to help prevent tip splitting. This shape concentrates the arc for accurate, deep fusion. For DCEP-only TIG, use a larger tungsten and let the end form a small, even ball. Current capacity is still limited because the electrode runs as the anode. On modern inverter AC for aluminum, a truncated point—not a large ball—often produces a tighter arc and better control because the machine limits EP time and protects the tungsten.
- Approximate current ranges with argon and electrode-negative polarity: 1/16 in (1.6 mm) up to ~90 A; 3/32 in (2.4 mm) up to ~180–200 A; 1/8 in (3.2 mm) up to ~250–300 A.
- DCEP capacity is roughly a fraction of DCEN capacity; a 3/32 in (2.4 mm) tungsten may tolerate only ~30–40 A EP before overheating.
- Helium mixes put more heat into the work but can make the arc less stable, so adjust gas flow and tungsten size.
When to Use DCEN vs DCEP on Real Jobs
For almost all TIG work on ferrous and high-temperature alloys, electrode-negative polarity is the default. It gives you efficient heat input, crisp arc control, and strong fusion while putting less stress on the electrode. DCEP is a niche setting that is most useful for cathodic cleaning on aluminum surfaces or for extremely thin aluminum sheet where you need to limit penetration. Most production aluminum work uses AC, which cycles between EN (penetration) and EP (cleaning) and lets you adjust the balance on an inverter. This quick-use guide is simple: use DCEN for penetration, AC for normal aluminum work, and DCEP only when you have a specific reason.
- Choose DCEN for: carbon steel, stainless steel, titanium, nickel alloys, most copper alloys, and structural joints where penetration matters.
- Use DCEP briefly to: remove stubborn oxide from aluminum, touch up an etch zone, or work on ultra-thin aluminum foil at very low amperage.
- Select AC for: general aluminum and magnesium work; set inverter balance to about 65–75% EN as a starting point for good penetration with enough cleaning.
- For thick aluminum or dirty castings: AC with more cleaning time, or EP, plus proper precleaning is usually more effective than DCEP alone.
Setting Up Your TIG Machine for the Right Polarity
Machine layout varies, but the basic connections stay the same. For DCEN, connect the TIG torch lead to the negative (-) terminal and the work lead to the positive (+) terminal. For DCEP, reverse those connections. Select DC on the process switch and use high-frequency (HF) start if the machine has it, since that helps prevent tungsten contamination. Lift-arc can work, but it increases the chance of touching the tip. Set enough preflow and postflow to protect the tungsten and puddle during starting and crater fill. Check your machine manual as part of the setup guide because some controls and terminal markings vary.
- Confirm polarity: DCEN (torch - / work +) for most metals; DCEP (torch + / work -) only for specialized cleaning or very thin aluminum.
- Set current mode: DC for steel; AC for aluminum and magnesium unless you have a specific reason to use DCEP.
- Choose tungsten type and size: lanthanated or ceriated for DCEN; use a larger diameter for any EP exposure.
- Prepare the tip: use a long taper with a small flat for DCEN, a small smooth ball for DCEP-only, and a truncated point for inverter AC.
- Install a gas lens and suitable cup, such as #7 to #12, based on the joint and stickout.
- Set shielding gas: pure argon is the baseline; start around 15–20 cfh (7–10 L/min) and adjust for cup size and the gas lens. Increase flow slightly for helium mixes or larger cups.
- Typical starting settings for mild steel, DCEN, and a 1/8 in joint: 3/32 in tungsten, 120–140 A, 15–18 cfh argon, and 1/2 in stickout with a gas lens.
- Typical starting settings for aluminum, AC inverter, and 1/8 in plate: 3/32 in tungsten, 130–160 A, 65–75% EN balance, 120 Hz, and 18–22 cfh argon.
- If you try DCEP for cleaning: use a large tungsten, such as 1/8 in, limit current to about 20–30 A, and watch the electrode temperature closely.
Shielding Gas, Arc Starts, and Torch Technique by Polarity
Shielding gas affects both heat input and arc stability. Pure argon gives smooth starts and a stable arc with DCEN or DCEP. Helium and argon/helium blends can add heat to thicker sections or support faster travel, but helium makes starting harder and can widen the arc. HF start is strongly recommended to preserve tip geometry with DCEN and provide reliable ignition. Scratch start risks tungsten contamination and arc wander. Hold the torch at a 10–15° angle and keep the arc short and consistent. That tightens the arc and limits porosity, which matters even more with the wider arc common to DCEP and AC EP. The practical technique guide is straightforward: control the arc length first, then adjust gas flow and travel speed.
- DCEN technique: keep the arc short, about one tungsten diameter, use a push or slight push angle for better gas coverage, and add filler to the leading edge of the puddle.
- DCEP technique: expect a wider, softer arc; reduce current, increase tungsten size, shorten the arc, and watch the etch zone so you don’t over-clean the surface.
- With AC on aluminum: adjust balance to avoid an excessively wide etch zone. Too much EP overheats the tungsten and weakens arc focus.
- Consider a gas lens and larger cup when extended stickout helps you see a fillet or inside corner.
Troubleshooting by Polarity: Symptoms and Fixes
Polarity errors and mismatched settings usually show up in the puddle or on the electrode. With DCEN, common problems include tungsten contamination from a long arc or poor grind, arc wander from weak gas coverage or magnetic arc blow, and undercut from moving too fast. With DCEP, the usual trouble is rapid tungsten overheating, uncontrolled ball growth, shallow penetration, and an etch zone that spreads too far across the aluminum. Run through these quick troubleshooting guide checks before you start chasing less obvious variables.
For DCEN:
- Tungsten contamination or spitting: shorten the arc, use HF start, add a small flat to the point, and verify gas coverage with a gas lens.
- Arc wandering: grind lengthwise rather than around the circumference, reduce stickout, increase cup size or flow, and remove drafts.
- Lack of penetration: increase amperage or preheat, slow your travel, or try a helium mix; also confirm fit-up and cleanliness.
- Undercut or a narrow bead: reduce travel speed and torch angle, add filler more often, and make sure heat input is adequate.
For DCEP:
- Tungsten overheating or excessive balling: lower amperage, use a larger tungsten, switch to AC with more EN time, and allow cooling pauses.
- Shallow penetration: switch to DCEN or AC. If DCEP is required, accept the limited penetration and adjust the joint design.
- Etch zone is too wide: reduce EP exposure with AC balance, lower current, or move faster to confine the cleaning action.
- Unstable arc starts: use HF start, make sure the ball is polished and symmetrical, and verify gas flow. Avoid helium-rich mixes at very low amperage.
FAQs About DCEN, DCEP, and AC Balance in TIG Work
Welders often ask how polarity changes with the alloy, joint type, and inverter features. Electrode-negative polarity remains the main setting for most TIG work, but knowing when EP helps can improve results on difficult aluminum surfaces. Inverter AC balance and frequency controls also reduce the need for dedicated DCEP because you can add enough cleaning without giving up as much penetration or electrode life. This FAQ guide covers the common points of confusion.
- Q: Can I TIG weld stainless with DCEP? A: No—use DCEN for penetration and arc focus; DCEP overheats the tungsten and reduces penetration.
- Q: Can aluminum be welded with DCEN only? A: It is possible with thorough mechanical or chemical cleaning and often helium mixes, but AC is preferred for consistent oxide removal.
- Q: Why is AC better than DCEP on aluminum? A: AC gives you EP for cleaning and EN for penetration, while balance control limits tungsten heating and keeps the puddle clean.
- Q: What is “straight” versus “reverse” polarity? A: Straight polarity is DCEN (torch -); reverse polarity is DCEP (torch +).
- Q: How does AC balance affect tungsten life? A: More EN, such as 65–75%, reduces EP time and keeps the tungsten cooler. Too much EP enlarges the ball and makes the arc less focused.
- Q: Does helium change the best polarity? A: No, but helium adds heat to the work and can improve penetration with DCEN. Use higher flow and expect harder starts.
- Q: What tip shape works best on inverters for aluminum? A: A truncated point resists balling, tightens the arc, and works well with an EN-heavy AC balance.
In short, DCEN is the go-to TIG polarity for strong penetration and a sharp, controllable arc on most metals. DCEP is a powerful but limited tool for cathodic cleaning and delicate, low-penetration work, and it is more commonly used as the EP half of AC on aluminum. Once you understand how polarity changes heat, arc shape, and tungsten behavior, this guide gives you a practical way to choose settings with more confidence, produce cleaner joints, and get longer life from the electrode.